Leveraging Technological Advancements in Recycling to Improve Efficiency and Reduce Costs in Australia

Recycling plays a vital role in Australia’s sustainable resource management, but traditional systems continue to face challenges such as contamination, inefficient sorting, and rising operational costs. As Australia works toward its waste reduction and resource recovery goals under the National Waste Policy Action Plan, technological advancements are creating new opportunities to improve recycling efficiency and economic performance. Technologies such as automated sorting systems, optical sensors, robotics, and data-driven solutions can help recycling facilities process materials more efficiently, reduce contamination, improve recovery rates, and minimise manual labour requirements. For Australian recycling operators, adopting these innovations can streamline processes while helping manage operational expenses. Understanding these technologies and their applications is therefore important for building more efficient and cost-effective recycling systems across Australia.
Recycling Technology SummaryAdvanced recycling technologies are helping Australian facilities improve sorting, material recovery, processing efficiency, and operational cost management. Automated systems, chemical recycling, AI, machine learning, IoT, and modern MRFs can support better material quality, throughput, maintenance, collection planning, and resource recovery. These technologies also contribute to circular economy goals by keeping materials in productive use. However, adoption requires investment, skilled workers, system integration, and regulatory alignment for effective implementation. |
Key Technological Advancements in Recycling
Automated Sorting Systems
Technology: Optical sorters, AI-powered robots, Near-Infrared (NIR) spectroscopy
Application: Separating and identifying mixed recyclable materials with greater accuracy.
Benefits:
- Improves sorting accuracy and material purity.
- Can improve recovery rates for targeted materials.
- Reduces reliance on manual sorting and associated labour requirements.
- Can help recover materials that are difficult to separate using conventional methods.
Chemical Recycling
Technology: Depolymerisation, pyrolysis, gasification
Application: Converts certain plastic waste into chemical feedstocks, monomers, or fuels.
Benefits:
- Can process certain contaminated or difficult-to-mechanically-recycle plastics into chemical feedstocks or fuels.
- Expands the range of plastics that can be recycled
- Reduces material going into landfill
Artificial Intelligence and Machine Learning
Technology: Machine vision, predictive analytics, real-time process optimisation
Application: Enhances sorting, process control, and facility management
Benefits:
- Can optimise material throughput and support improved recovery rates.
- Can reduce downtime and maintenance costs through predictive maintenance.
- Enhances decision-making and reporting through real-time data
- Can monitor and control the processing plant’s performance
Internet of Things (IoT) in Waste Collection
Technology: Smart bins, GPS-enabled fleet tracking, sensor networks, route optimisation software
Application: Monitors waste levels, collection patterns, bin contamination, and collection routes
Benefits:
- Optimises collection routes, reducing fuel and labour costs
- Prevents bin overflow and contamination
- Enables data-driven waste policy decisions
Advanced Material Recovery Facilities (MRFs)
Technology: Robotics, AI, NIR sorting, and conveyor automation
Application: Processes single-stream and complex waste streams using integrated automated technologies
Benefits:
- Can improve recovery and material purity rates through advanced sorting technologies
- Reduces operational costs through automation
- Captures performance data for monitoring and reporting
- Monitors and controls the plant’s performance
- Supports circular economy initiatives by producing clean recyclables
Improve commercial and industrial waste management with practical solutions designed to support efficient operations, resource recovery, and sustainability across Australia! |
Benefits of Technological Adoption in the Recycling Sector
Category | Benefits |
Efficiency | Higher throughput, fewer bottlenecks, faster processing |
Cost Reduction | Potentially lower labour, energy, and maintenance costs over time |
Material Quality | Cleaner, higher-quality outputs with greater potential market value |
Environmental Impact | Potentially less landfill waste, emissions, and energy consumption |
Data-Driven Management | Better traceability, compliance, and planning |
Resilience and Scalability | Adapts to fluctuating input volumes and material types |
Australia recycled or reused approximately 47.6 million tonnes of waste materials in 2022–23, demonstrating the scale of resource recovery across the country.
How Recycling Technology Supports a More Circular Economy in Australia
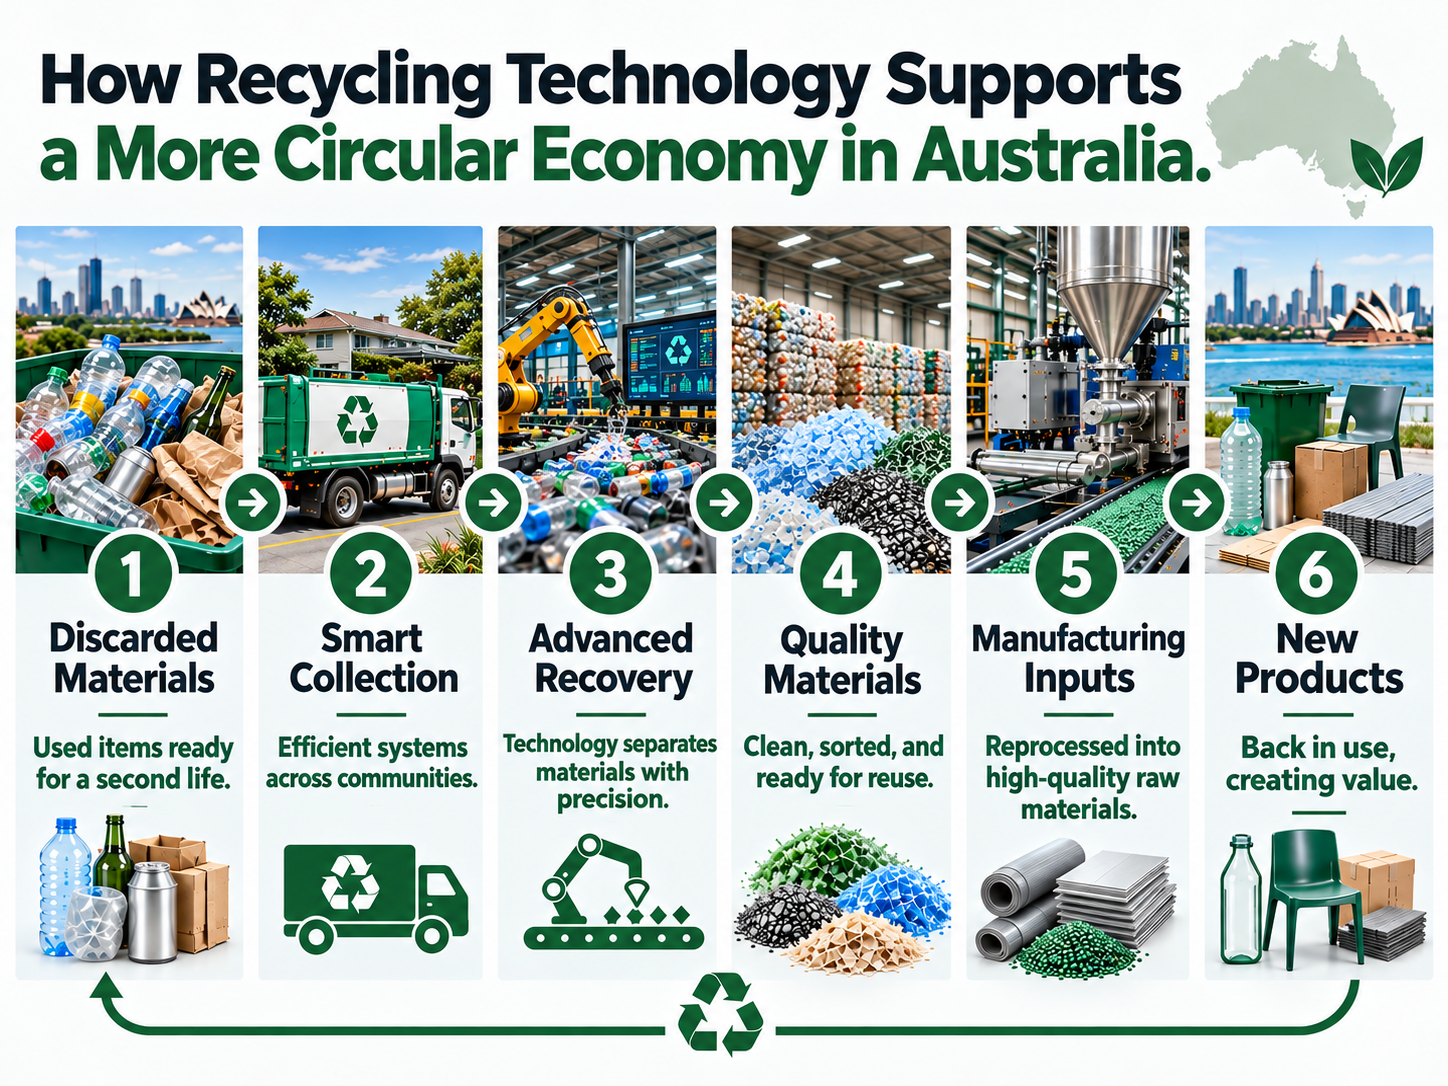
Recycling technology can help Australia move beyond simply managing waste toward keeping valuable materials in use for longer. By connecting collection, recovery, processing, and manufacturing, modern recycling systems can help return recovered resources to productive use. The infographic below illustrates this circular pathway, showing how technology can support resource recovery, reduce material loss, and strengthen a more sustainable approach to Australia’s waste management. Australia’s 2024 National Waste Policy Action Plan supports resource recovery with the transition to a circular economy, with a target of achieving an 80% average resource recovery rate from all waste streams by 2030.
Challenges and Considerations
While technological adoption can bring significant benefits, the recycling solutions industry must navigate several challenges:
- High initial capital costs
- Need for skilled workforce
- Integration with legacy systems
- Regulatory alignment and standards
Waste management responsibilities are shared across Australian governments, with state and territory frameworks covering areas such as legislation, regulation, planning, transport, treatment and disposal. Government incentives, public-private partnerships, and workforce development will be essential to overcoming these barriers in Australia.
Conclusion
The integration of advanced recycling technology offers Australia a pathway to a more efficient, cost-effective, and environmentally sustainable waste management system. As recycling facilities look to modernise their operations, OGTEC provides advanced recycling and waste management solutions designed to improve processing efficiency, optimise resource recovery, and support evolving operational needs. By investing in innovations such as AI-powered sorting, chemical recycling, and IoT-enabled collection, the recycling industry can significantly improve resource recovery rates, lower operational costs, and contribute to a circular economy. Continued collaboration between government, industry, and technology providers will be key to scaling these innovations and meeting Australia’s national waste and climate targets.
Improve recycling efficiency, optimise resource recovery, and build smarter operations with OGTEC’s tailored waste and recycling solutions! |
Frequently Asked Questions About Recycling Technology
Q1. How can recycling technology be integrated into an existing waste processing facility?
Integration typically involves assessing current equipment, identifying process gaps, upgrading compatible systems, installing new technology in stages, and testing performance before full implementation to minimise operational disruption.
Q2. What role does real-time data play in improving recycling facility performance?
Real-time data helps operators identify process inefficiencies, track equipment performance, monitor material flows, detect operational changes, and make timely adjustments that support consistent facility performance and informed planning.
Q3. Why is staff training important when introducing new recycling equipment?
Staff training ensures operators understand new equipment, control systems, safety procedures, and maintenance requirements. Proper training can also help facilities use new technology effectively and identify operational issues promptly.
Q4. Can recycling technology be upgraded as facility requirements change?
Many modern recycling systems can be configured or expanded as processing requirements evolve. Facilities should consider modular equipment, compatible controls, and future capacity needs when planning technology investments.
Q5. How can recycling facilities minimize disruption during technology upgrades?
Facilities can introduce upgrades in planned stages, schedule installation during maintenance periods, maintain essential processing capacity, and test new equipment before transitioning fully to the upgraded system.